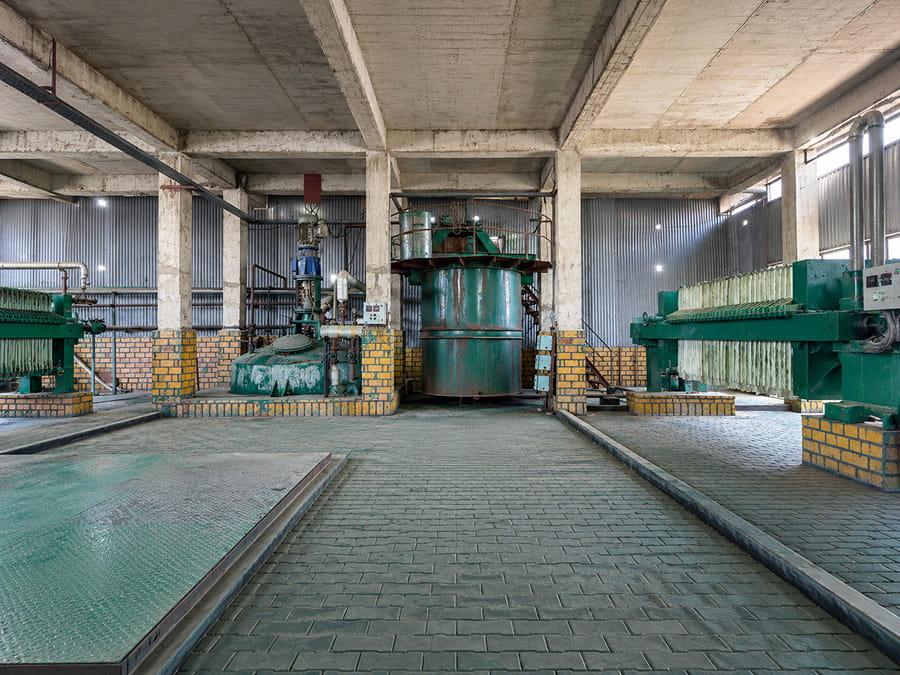
State-of-the-Art Manufacturing Infrastructure
100% In-House Manufacturing
10 pigment categories manufactured in-house in Lucknow, India.
Manali Pigments Private Limited manufactures all 10 pigment categories in-house at its facility in Lucknow, India. Direct control of production, application testing and dispatch supports consistent industrial pigment supply for paints, plastics, printing inks, rubber, textiles and construction. Our manufacturing team brings over 36 years of experience serving global buyers.
This infrastructure powers our manufacturing excellence philosophy—complete vertical integration from raw material to finished pigment.
The In-House Manufacturing Advantage
Our infrastructure is designed to solve the critical challenges faced by procurement managers and technical specialists across the paints, plastics, inks, and construction industries.
Controlled Batch Consistency
In-house synthesis, processing and quality checks help maintain pigment shade and strength within grade-specific requirements. Buyers should evaluate the relevant technical data and batch documentation for their application. Checks operate within our ISO 9001:2015 quality framework.
Direct Production and Supply Coordination
Direct control of manufacturing schedules supports supply planning without reliance on third-party pigment sourcing. Order quantities, production availability and shipment timing are confirmed for each requirement.
Application-Led Technical Support
Our manufacturing and application-lab teams evaluate pigment requirements for the intended system. Share the substrate, processing conditions and performance targets so grade selection and trial priorities can be agreed, including thermal stability testing for masterbatch applications where relevant.
Advanced Production Stages
Our facility utilizes industry-leading equipment, strictly monitored through defined Standard Operating Procedures (SOPs) to ensure the highest purity and performance.
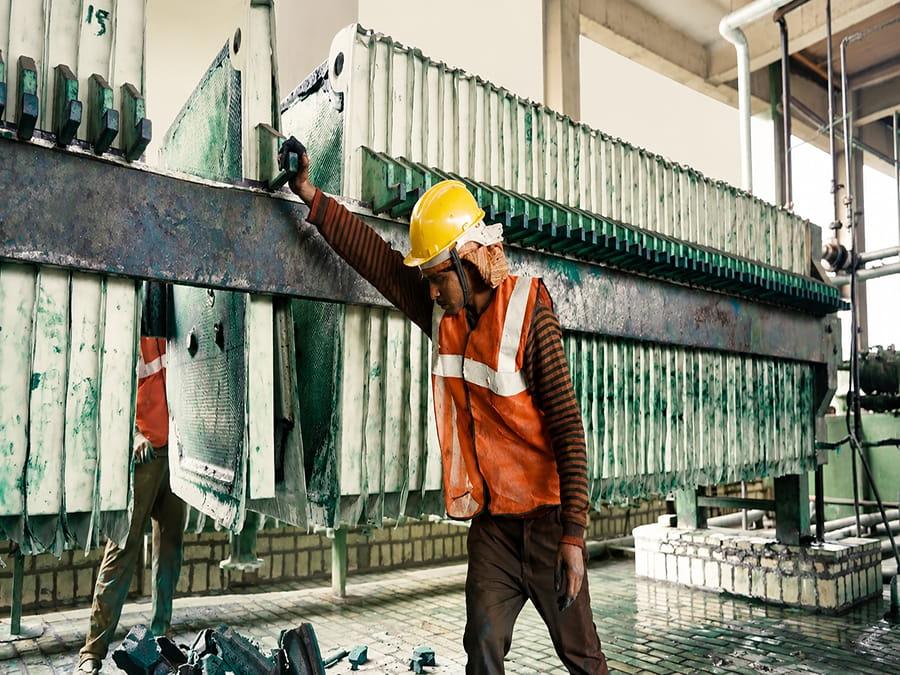
Stage 1: Synthesis & Filtration
Hydraulic filter presses support washing and filtration during pigment production. These controlled processing stages form part of our in-house manufacture of Organic Azo pigments and Phthalocyanine Blue & Green pigments. Grade-specific processing and quality checks support consistent material preparation for subsequent production stages.
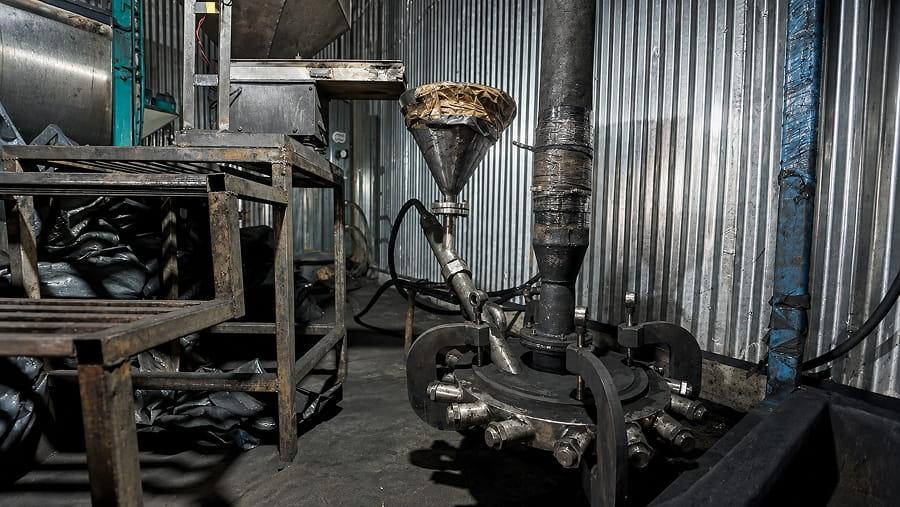
Stage 2: Milling & Dispersion
Air classifier and jet milling equipment support pigment particle-size control for the relevant grades. Milling helps prepare powder for use in a formulation; final dispersion performance also depends on the binder, additives, loading and processing conditions of the customer's system.
Controlled micronization supports grade-specific Chrome Oxide Green applications where particle-size requirements are important.
Integrated R&D and Application Testing
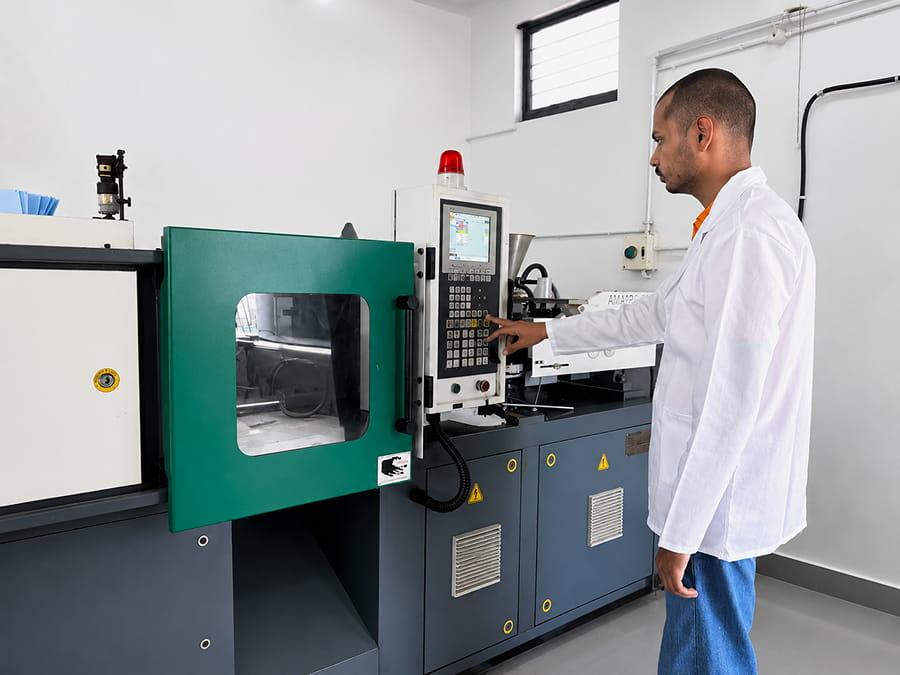
Technology is only as effective as the testing behind it. Our in-house R&D laboratory simulates production conditions to evaluate performance before dispatch. Using equipment such as the High Speed Disperser and Injection Moulding machines, relevant parameters such as heat stability for plastics, color fastness for textiles and dispersion quality for printing inks can be assessed. Results are grade- and system-specific, so we recommend confirming them through trials in your own process.
Dedicated testing also supports the performance requirements of cement and concrete pigmentation.
Evaluate the relevant pigment grade in your own application.
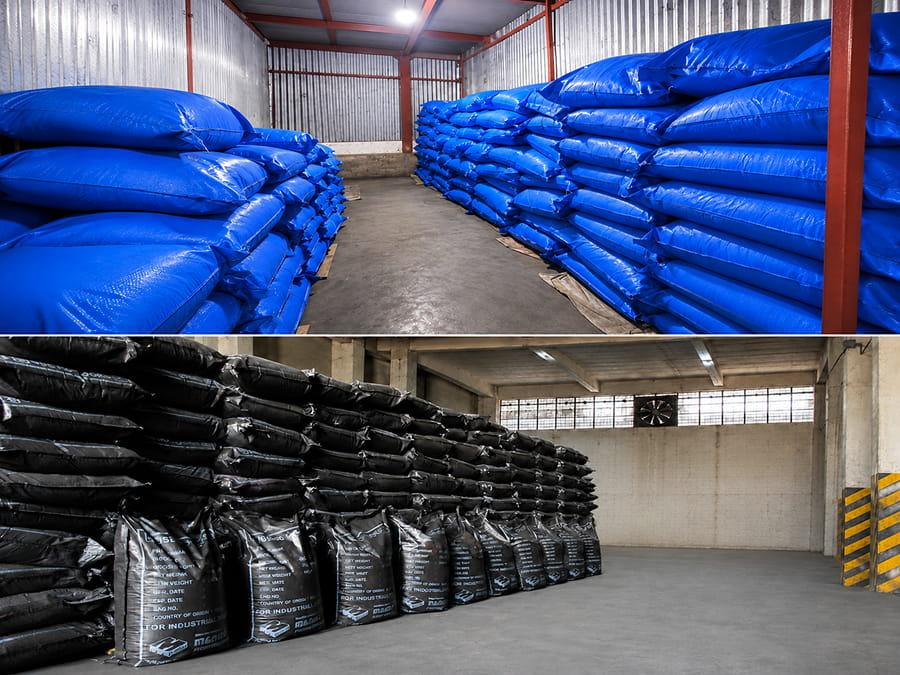
Traceability and Global Dispatch
Seamless logistics are integral to our manufacturing excellence. Our organized material handling and storage systems support batch traceability from the receipt of raw materials to final delivery. Operating as a recognized STAR EXPORT HOUSE, our facility features segregated storage and safe handling protocols designed for international scale. This approach allows us to serve over 15 countries, providing our global partners with the documentation and consistency they require.
Certifications & Standards
Our manufacturing systems combine documented process control, export readiness, and defined operating procedures to support consistent industrial pigment supply.
ISO 9001:2015
Our quality-management system certification covers documented process control, checks and consistent execution across manufacturing activities. It describes the management system, not an approval of any individual product.
Government of India Recognised STAR EXPORT HOUSE
This is an export recognition reflecting the company's export performance and international trading capability. It is not a product-quality certificate or a regulatory approval for any application or destination market.
Frequently Asked Questions
Yes. Manali Pigments Private Limited manufactures its industrial pigment portfolio in-house across 10 categories at its facility in Lucknow, India. The manufacturing team controls production, application testing and dispatch rather than sourcing finished pigments from third-party manufacturers.
In-house processing and quality checks support control of pigment shade, strength and relevant grade specifications. Buyers should review the technical data and batch documentation for their selected grade and validate performance in their own formulation. Controlled production does not mean every pigment or application has identical test requirements.
Manali Pigments operates under an ISO 9001:2015 quality-management framework and holds Government of India Recognised STAR EXPORT HOUSE status. ISO certification concerns the quality-management system; STAR EXPORT HOUSE is an export recognition. Neither is a blanket approval for every product, application or destination-market regulation.
Yes. The application laboratory uses equipment including high-speed dispersion and injection moulding to evaluate relevant pigment requirements. Share the binder or polymer, processing conditions and performance targets. Heat stability for plastics, dispersion for inks, fastness for textiles or rubber, and weathering or alkali resistance for construction require grade- and application-specific assessment and customer trials.
Air classifier and jet milling equipment support particle-size control for relevant pigment grades. Milling prepares powder for subsequent use, but final dispersion depends on the formulation, binder, additives and processing conditions. A milled pigment powder should not be treated as automatically equivalent to a ready-to-use pigment dispersion.
Request the grade-specific Technical Data Sheet, Safety Data Sheet and relevant Certificate of Analysis or batch-test information. State the Colour Index, intended application and destination country so the team can identify applicable documentation. Regulatory or special-use declarations must be confirmed for the selected grade and market rather than assumed for the entire portfolio.
The manufacturing and storage systems maintain batch traceability from material receipt through processing and dispatch. Buyers should include the grade, batch reference and destination requirements when requesting quality or shipment documentation. Packaging, availability and shipment timing are confirmed against the particular order.
Yes. Use Schedule a Factory Visit to provide your company, country, email and preferred date; the team will coordinate and confirm availability. Use Request Product Samples to identify the category, grade if known, sample quantity and application. A submitted enquiry is a request for coordination, not an automatically confirmed visit or sample shipment.
Discuss your pigment supply requirements
Partner with a 100% in-house manufacturer for consistent quality and reliable global delivery.